About Industrial Cold Room Storage
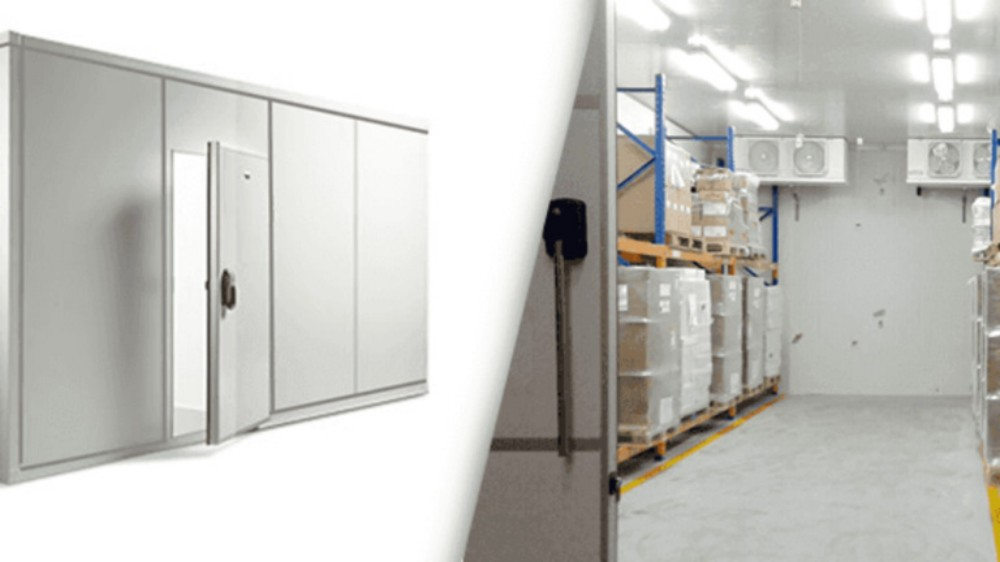
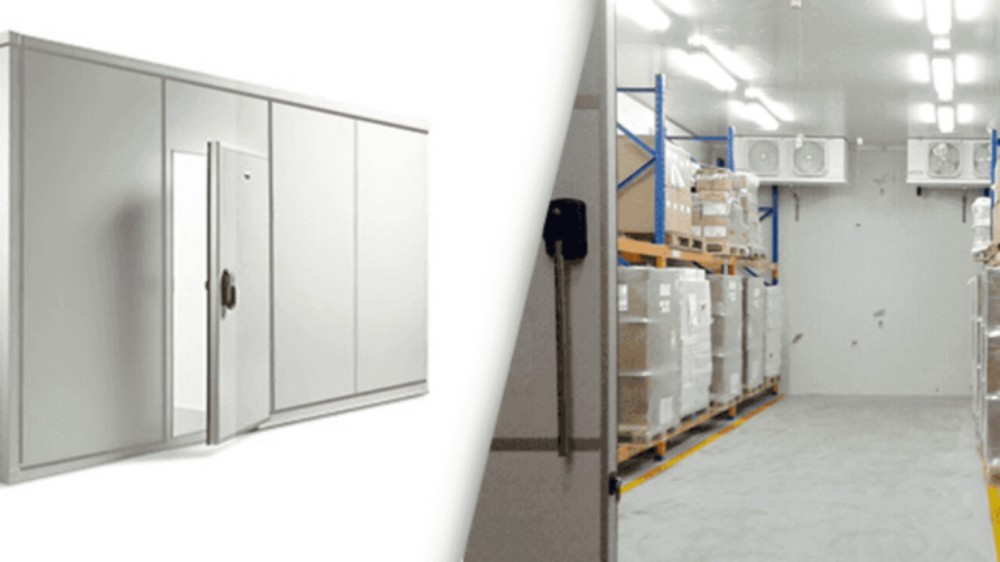
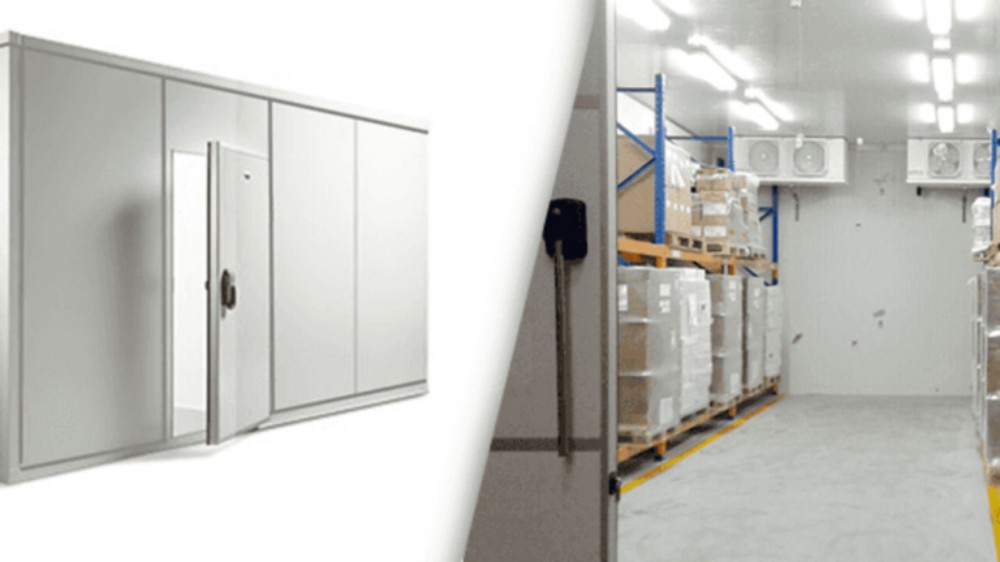
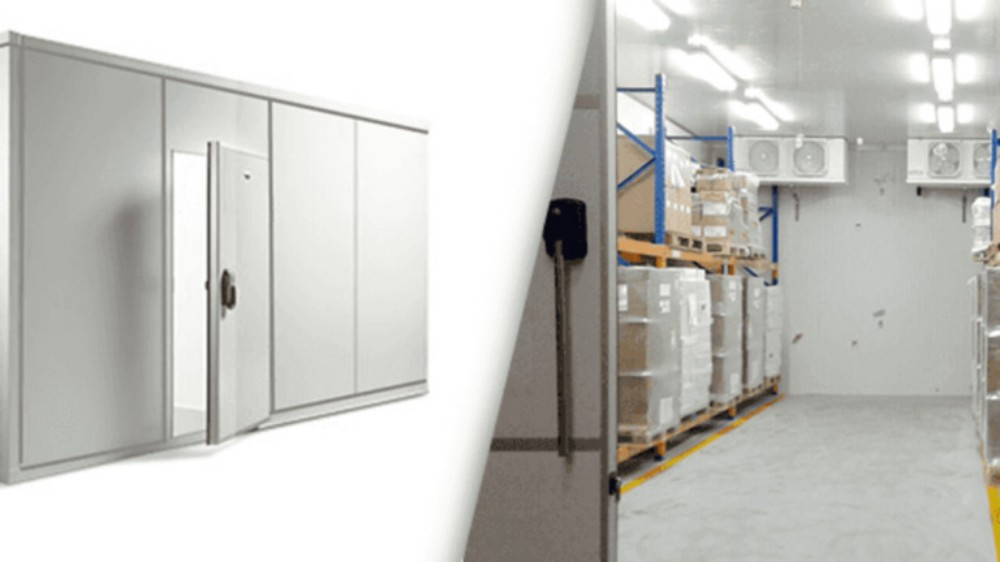
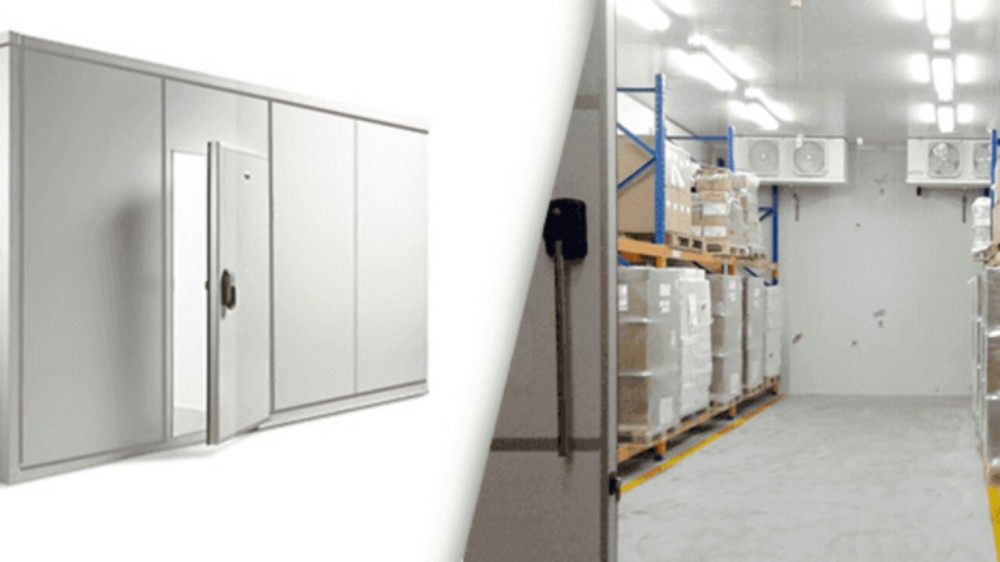
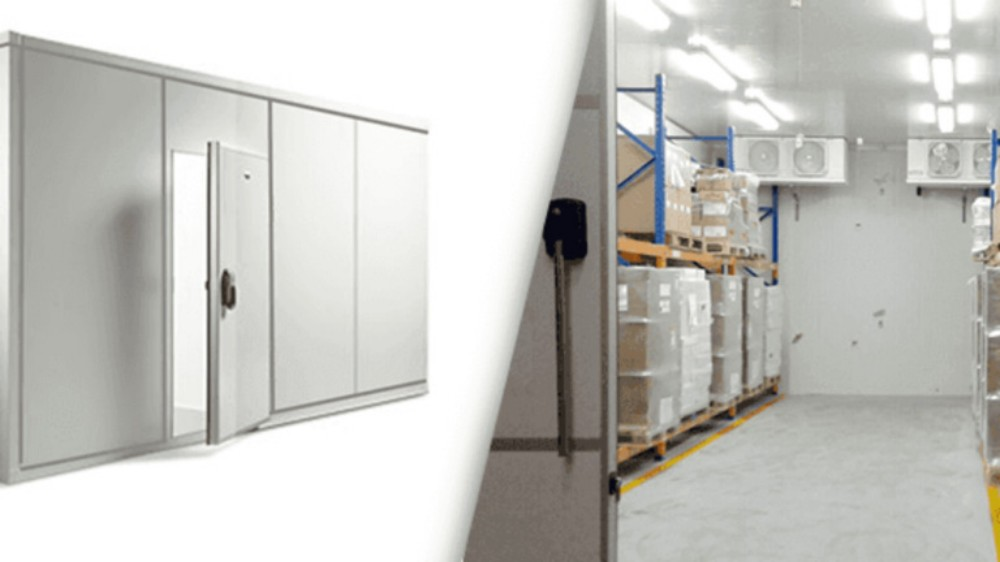
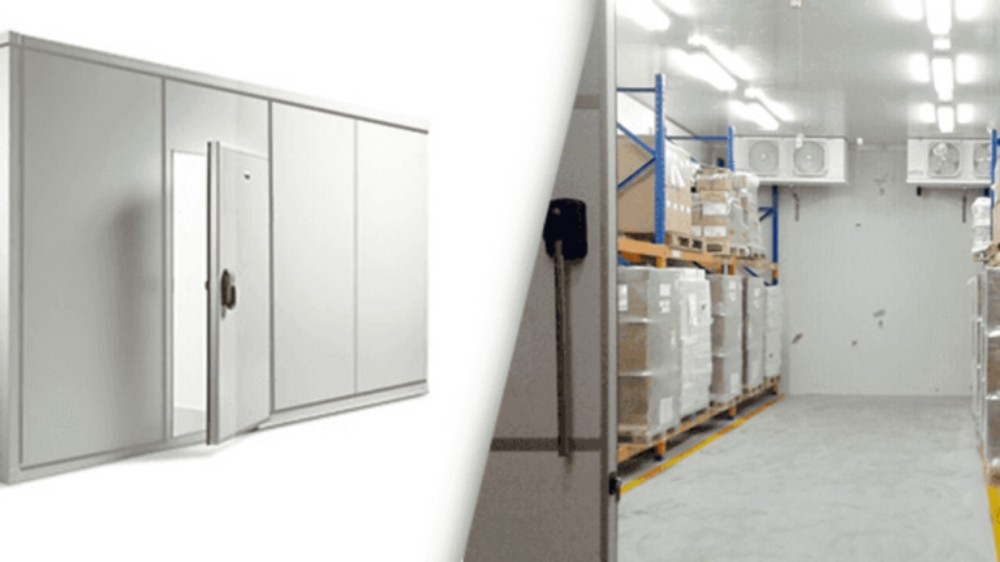
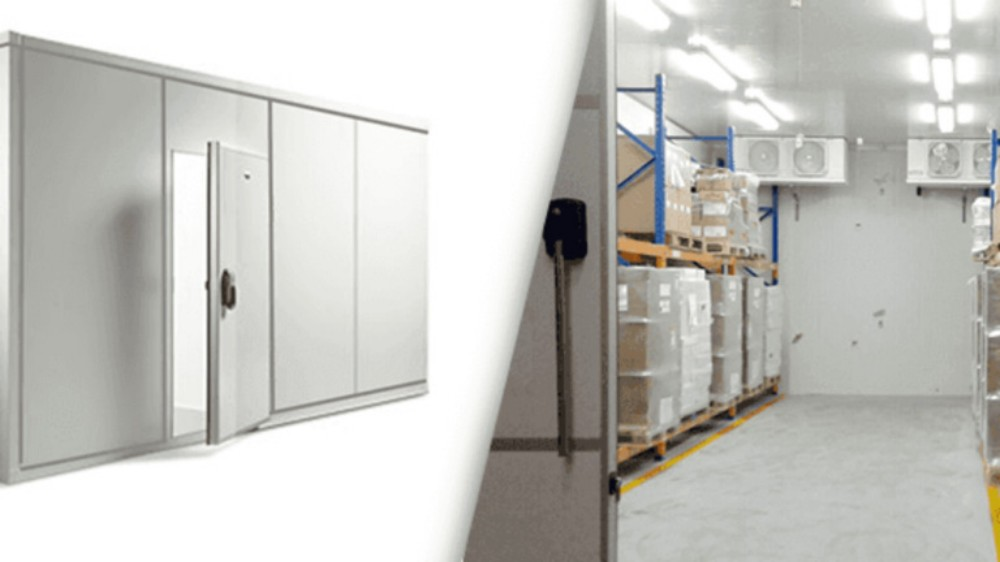
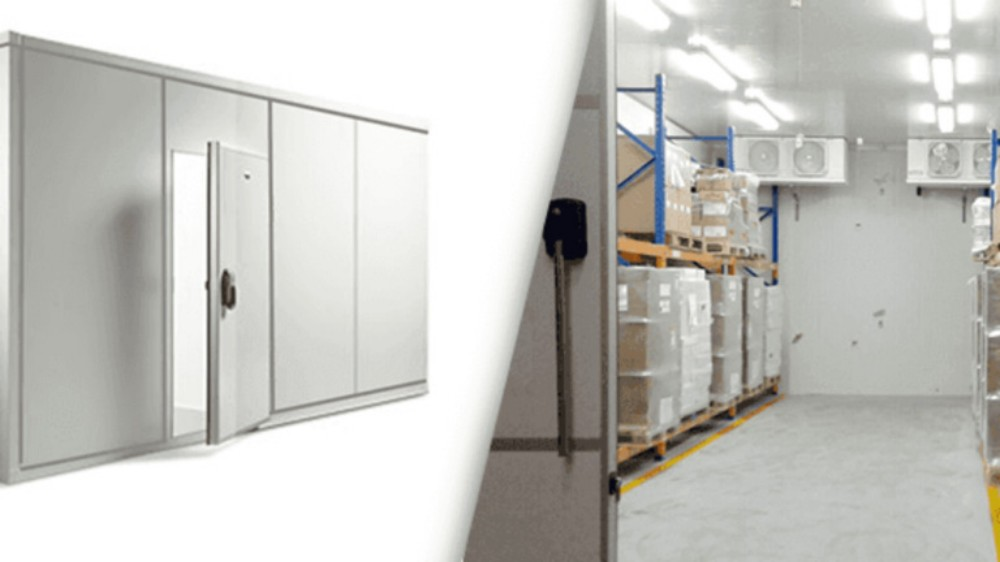
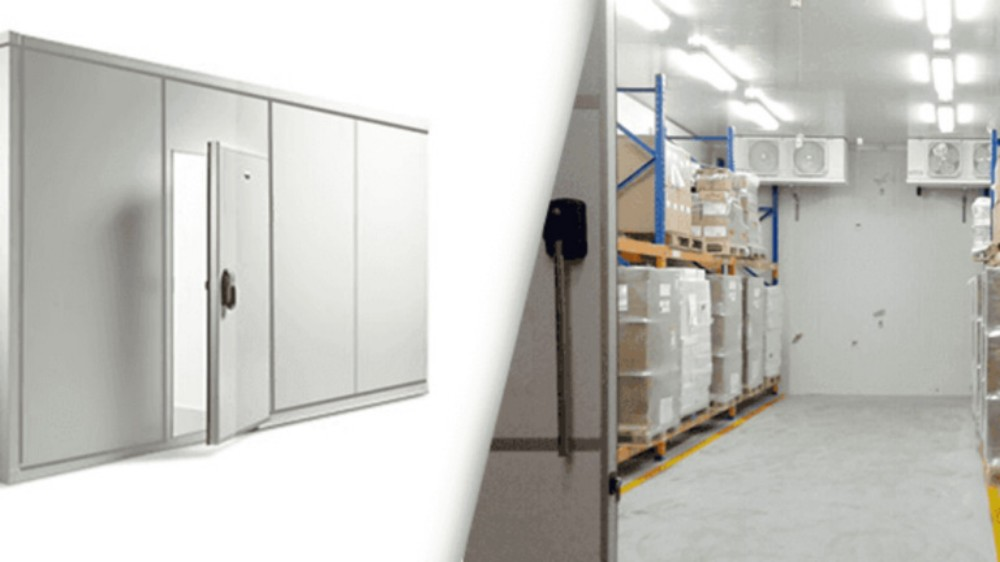
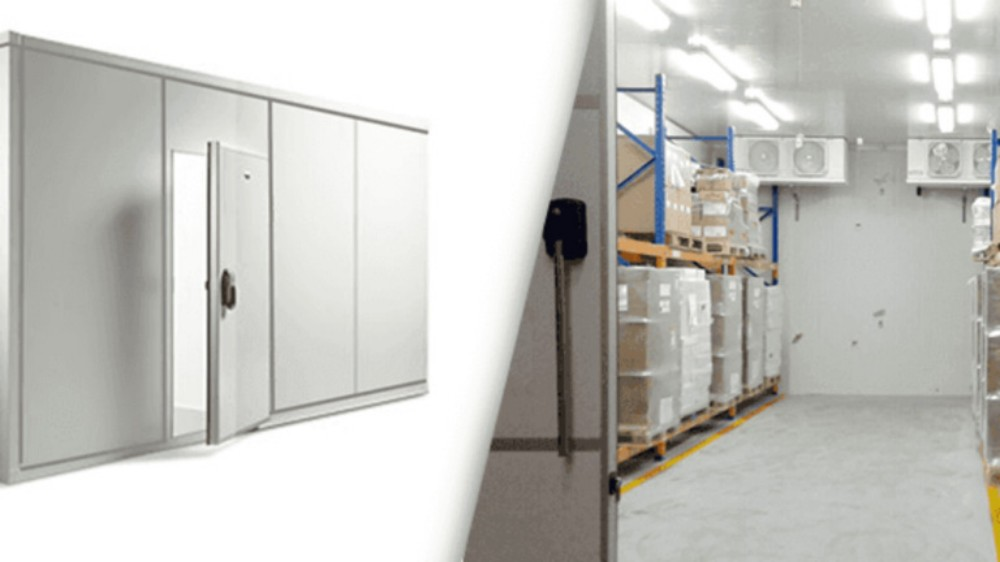
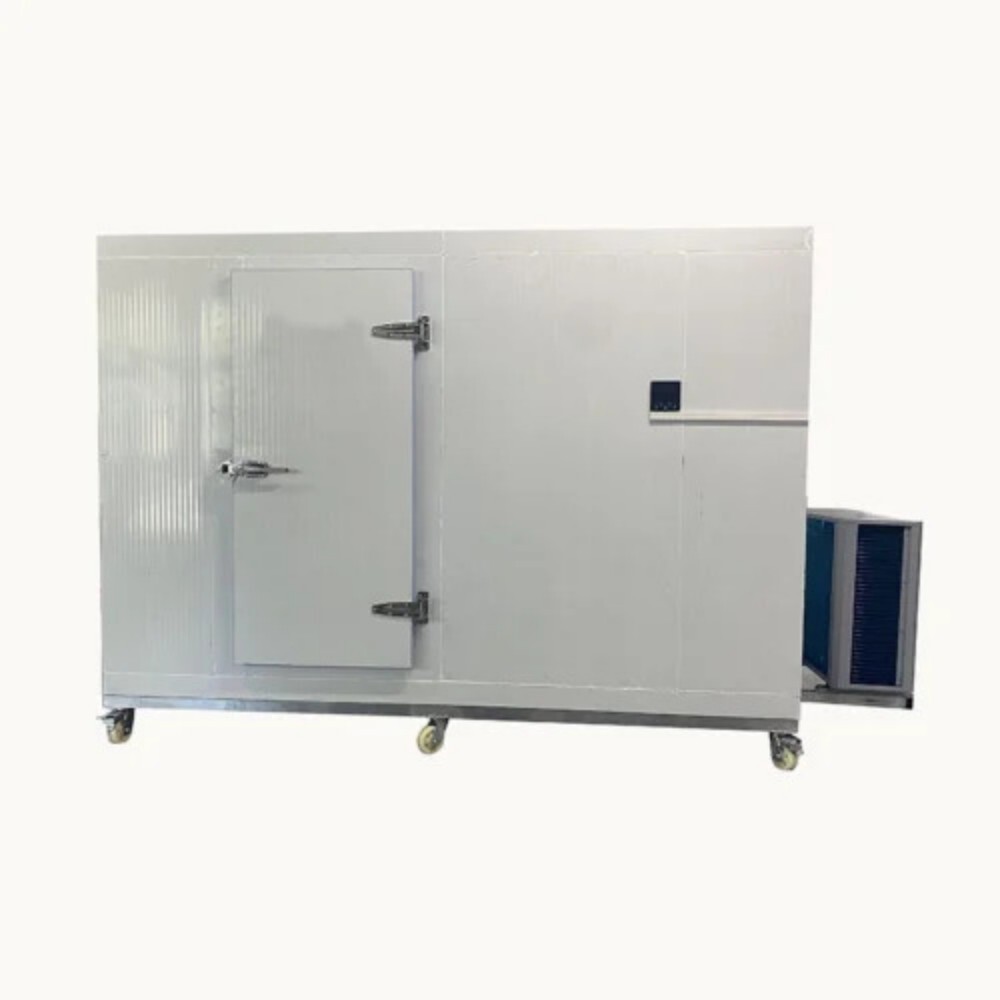
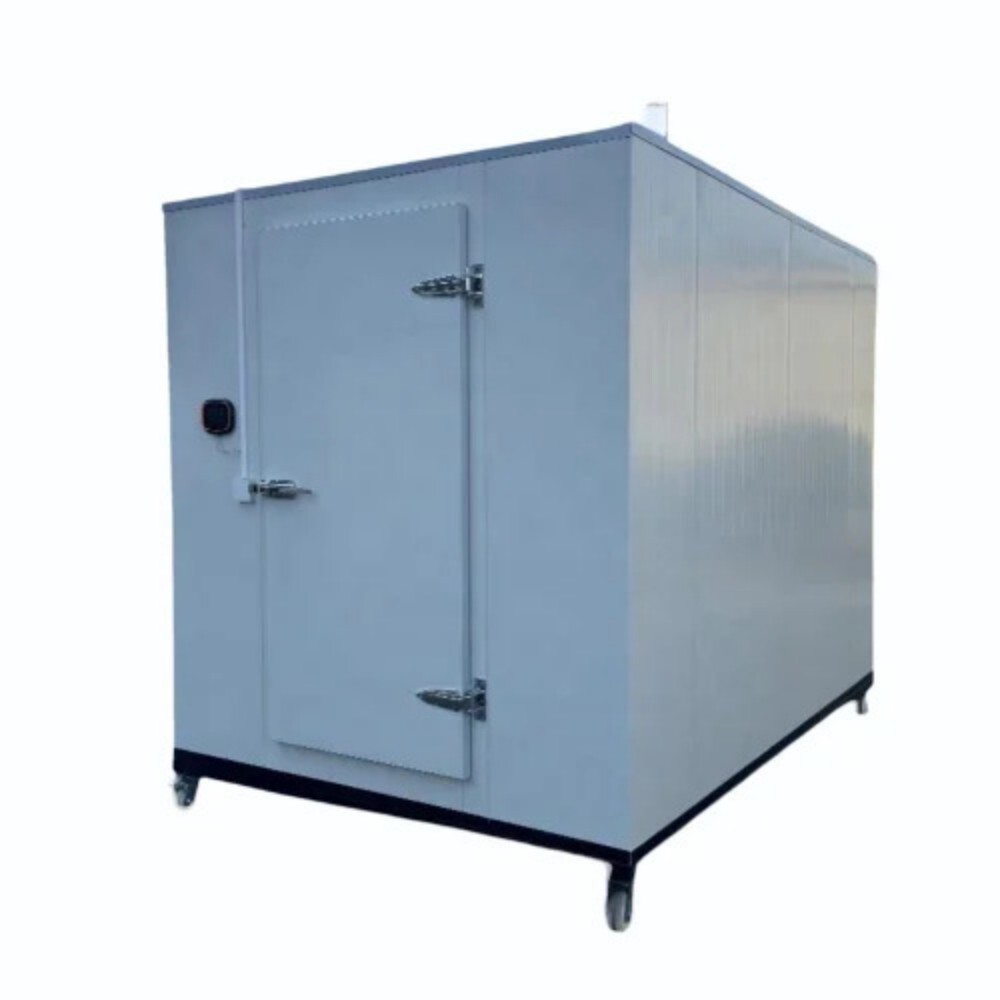
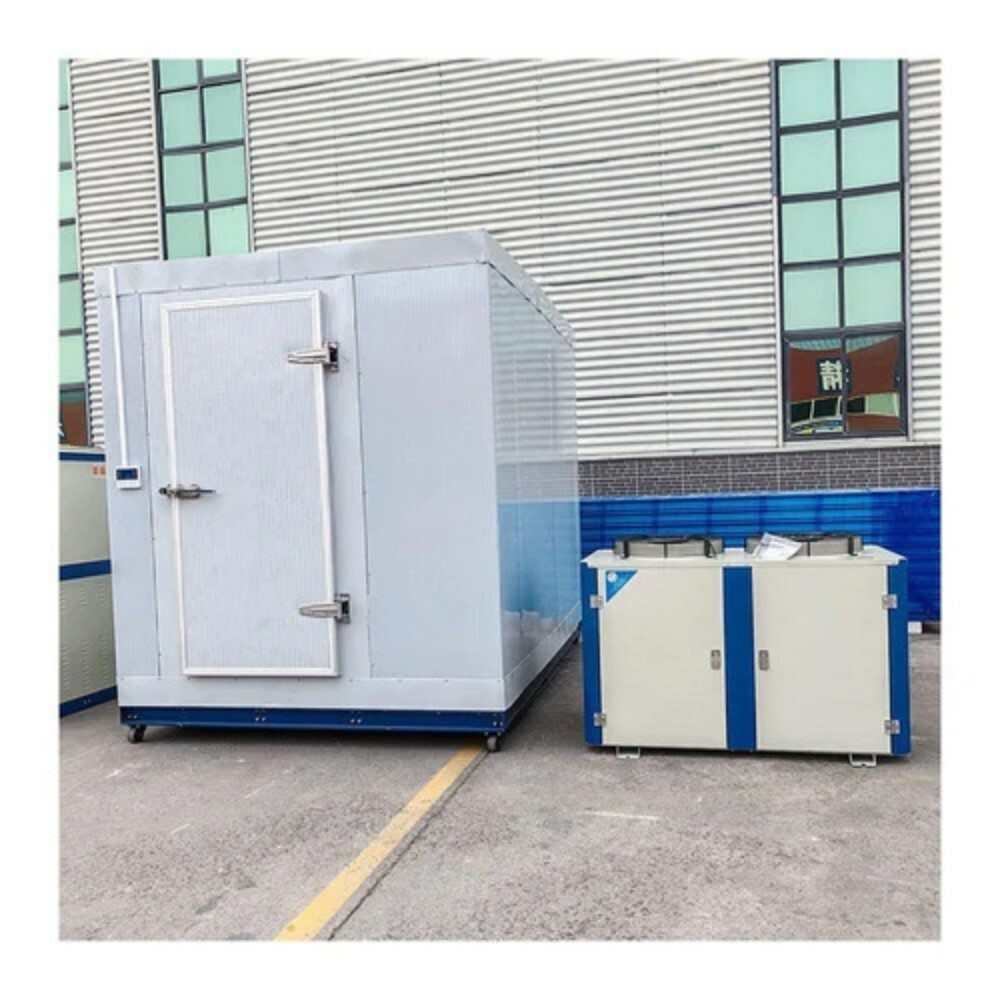
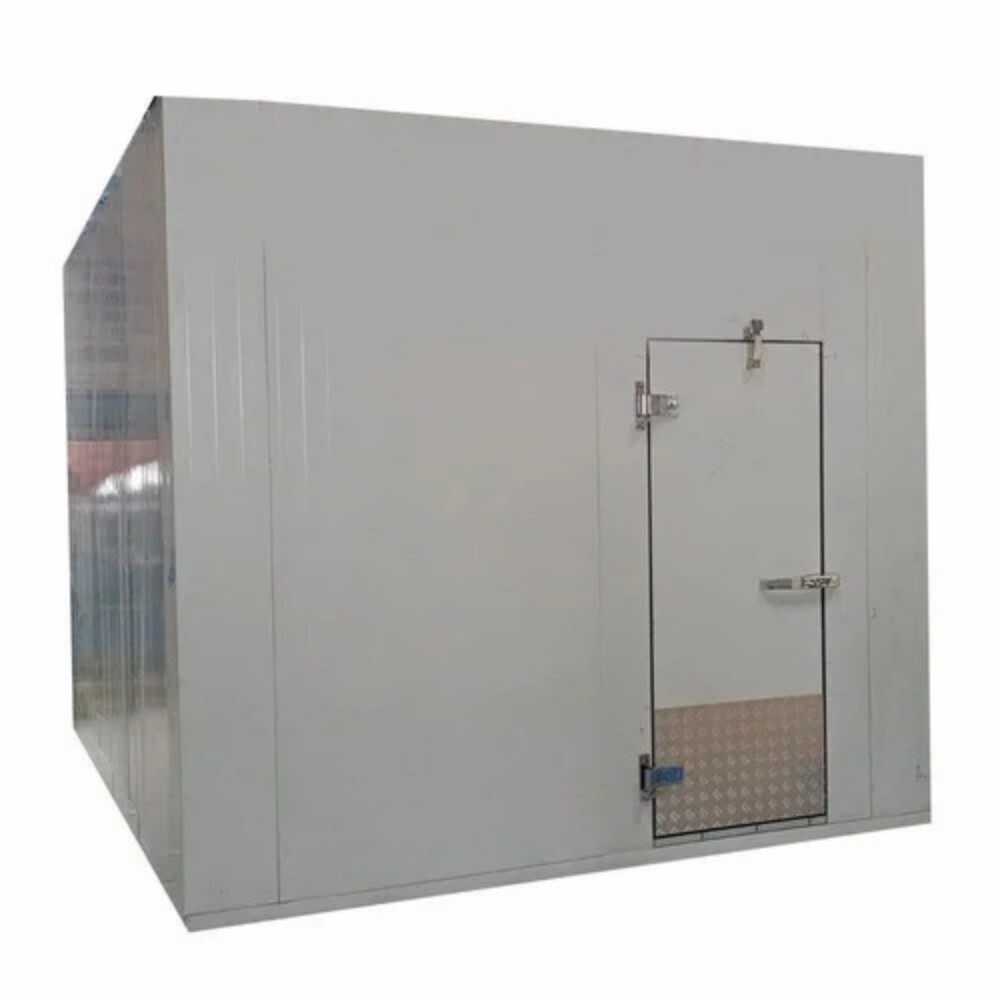
Experience opulent efficiency with our Industrial Cold Room Storage solutions-where cost-effective design meets spectacular performance. Choose panel thicknesses from 60 mm to 120 mm and refrigerant options like R404A, R134a, or R507. The modular installation, championed by our virtuoso engineering, ensures swift on-site assembly with seamless, airtight PU gasket sealing. Galvanized steel or stainless-steel shelving, LED safety lighting, and digital microprocessor controls deliver an ephemeral yet enduring storage environment. Create a secure, energy-efficient haven for food, pharma, or hospitality-order today for a truly premium solution.
Top-Tier Features & Versatile Applications
Industrial Cold Room Storage units excel in areas demanding reliable climate control such as food preservation, pharmaceutical warehousing, hospitality services, and industrial processing facilities. Designed for mounting on floors, walls, or ceilings, they offer customizable application surfaces with smooth or embossed finishes. Noteworthy extras include HACCP compliance, anti-bacterial and fire-resistant panels, energy-efficient lighting, and microprocessor-based digital controls. Optional galvanized or SS shelving amplifies versatility, supporting a broad spectrum of operational needs while maintaining opulent standards of hygiene and safety.
Swift Sample Policy & Efficient Delivery
We offer an ephemeral sample policy to let you assess our cold room quality firsthand. With quick dispatch and streamlined freight logistics, your units are delivered promptly to your site, whether as a drop-off or full installation service. Our robust supply ability ensures uninterrupted availability, guaranteeing your operations never face downtime. Delivery timelines vary by customization but generally range from days to a few weeks-always with a commitment to punctual, reliable handover, tailored for industries across India.
FAQ's of Industrial Cold Room Storage:
Q: How do I select the appropriate cold room configuration for my needs?
A: Choosing the right configuration depends on your storage requirements, desired temperature range, capacity, and application area. Our team provides consultation to recommend optimal panel thickness, refrigerant type, and shelving based on industry standards and your specific needs.
Q: What is the process for installation and commissioning?
A: Our industrial cold rooms utilize a modular design for swift on-site installation by skilled technicians. The process includes assembling panels, integrating the refrigeration system, testing the airtight seal, calibrating the digital controller, and conducting a thorough quality check before handover.
Q: When can I expect delivery after placing an order?
A: Delivery time depends on specification and order size, but most standard cold rooms are dispatched within 10-28 days. We prioritize quick dispatch and efficient freight coordination to ensure a seamless drop-off or installation at your premises.
Q: Where can these cold room storages be used?
A: Our cold rooms are suitable for diverse applications including the food industry, pharmaceutical storage, hospitality establishments, and industrial processing. Designed to adapt to various spaces, they can be floor, wall, or ceiling mounted to suit unique site requirements.
Q: What benefits do anti-bacterial and fire-resistant panels provide?
A: Anti-bacterial and fire-resistant panels enhance safety and hygiene by limiting bacterial growth and offering protection against fire hazards. These features are essential for environments with strict regulatory standards, such as food storage and pharmaceutical applications.

 Send Inquiry




 Send Inquiry


 Send Inquiry


